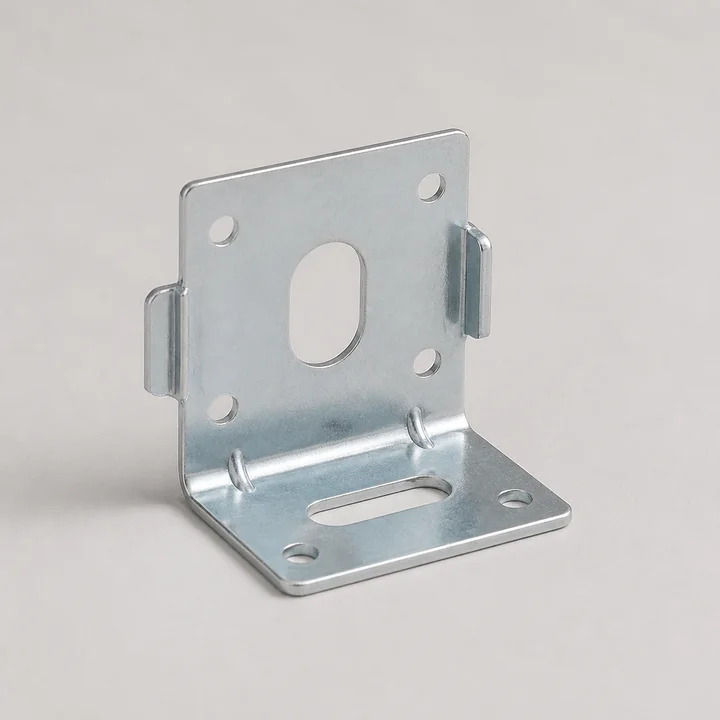
Meridian Control Panels builds custom UL-listed control panels for water-treatment and packaging OEMs. The parts that were slowing them down weren't complex — they were the dozens of simple right-angle brackets that stand components off the backplane, and they were making every one of them by hand.
A simple part, made the hard way
With fifteen people and a steady book of custom work, Meridian lives and dies by how quickly a panel moves from the print to the wire-out bench. Each enclosure needs ten to fifteen right-angle brackets to mount contactors, relays, and DIN rail off the backplane at the right standoff height.
For years those brackets were shop-made: shear a length of angle stock, mark it, drill the mounting holes, deburr, and set it aside. It worked when Meridian shipped a few panels a week. As the order book grew, that quiet little operation turned into the bottleneck nobody wanted to own.
Where the in-house bracket broke down
The real cost wasn't the cutting — it was the inconsistency. Hand-marked hole spacing drifted a millimeter here and there, so components didn't always line up cleanly on the rail, and assemblers lost time shimming and re-drilling. Every bracket also needed hand deburring before it touched a painted backplane, and the whole job tied up a skilled fabricator who should have been building enclosures.
Meridian sent us a sample bracket and a marked-up sketch and asked a straightforward question: can you just make these, to the same size, every time?
The part we built
We tooled a progressive-die stamping in 2.0mm 1008 cold-rolled steel, clear-zinc plated so it drops straight into a UL panel with no secondary finishing. Hole positions are held to ±0.10mm, and we added pierced adjustment slots so the same bracket covers several component heights instead of three separate shop-made variants.
The first article was inspected and approved before the tool ran production, and the tooling stays maintained on our floor for scheduled repeat orders. Meridian started at a few thousand pieces a year with room to scale into the tens of thousands as their volume grows.
What changed on the floor
Brackets now arrive plated, deburred, and identical. Assemblers pull them from a bin and fasten — no marking, no drilling, no shimming. The skilled fabricator who used to spend a chunk of every week on bracket prep went back to building panels, and fit-up rework on the rail effectively disappeared.
It's the least glamorous part in the enclosure, and it was quietly costing Meridian a day a week. Standardizing it bought that day back.
“We didn't think of a bracket as a bottleneck until Proco took it off our plate. Now they show up perfect and we just build.”
Dana Okafor, Operations Manager, Meridian Control Panels